Language
 中文简体
 English
 عربى
 русский

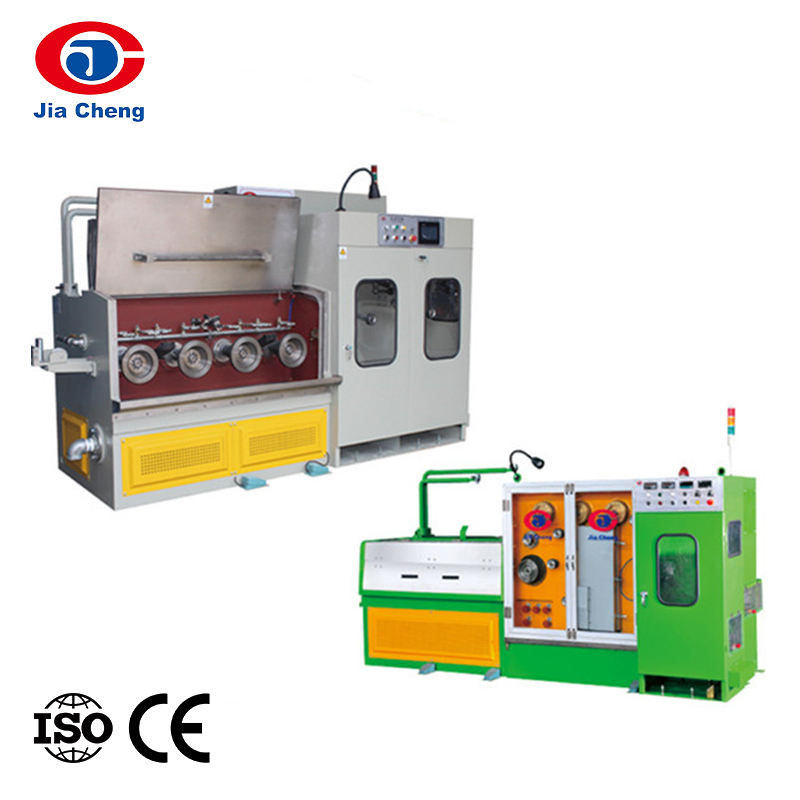
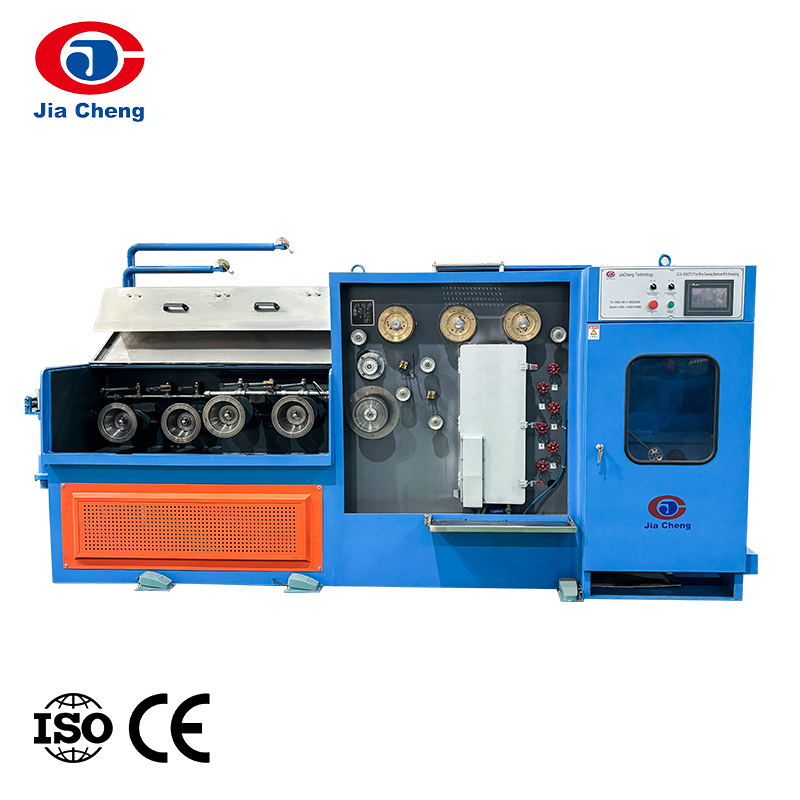
Typical Technical Parameters
Enameled wire equipment is judged on oven temperature control precision, coating uniformity, and line speed, since these three factors together determine both the finished wire's insulation performance and your production output. The table below gives typical ranges for the core machines in this category.
| Machine Type | Typical Product Range | Max Line Speed | Drive & Control | Typical Motor Power |
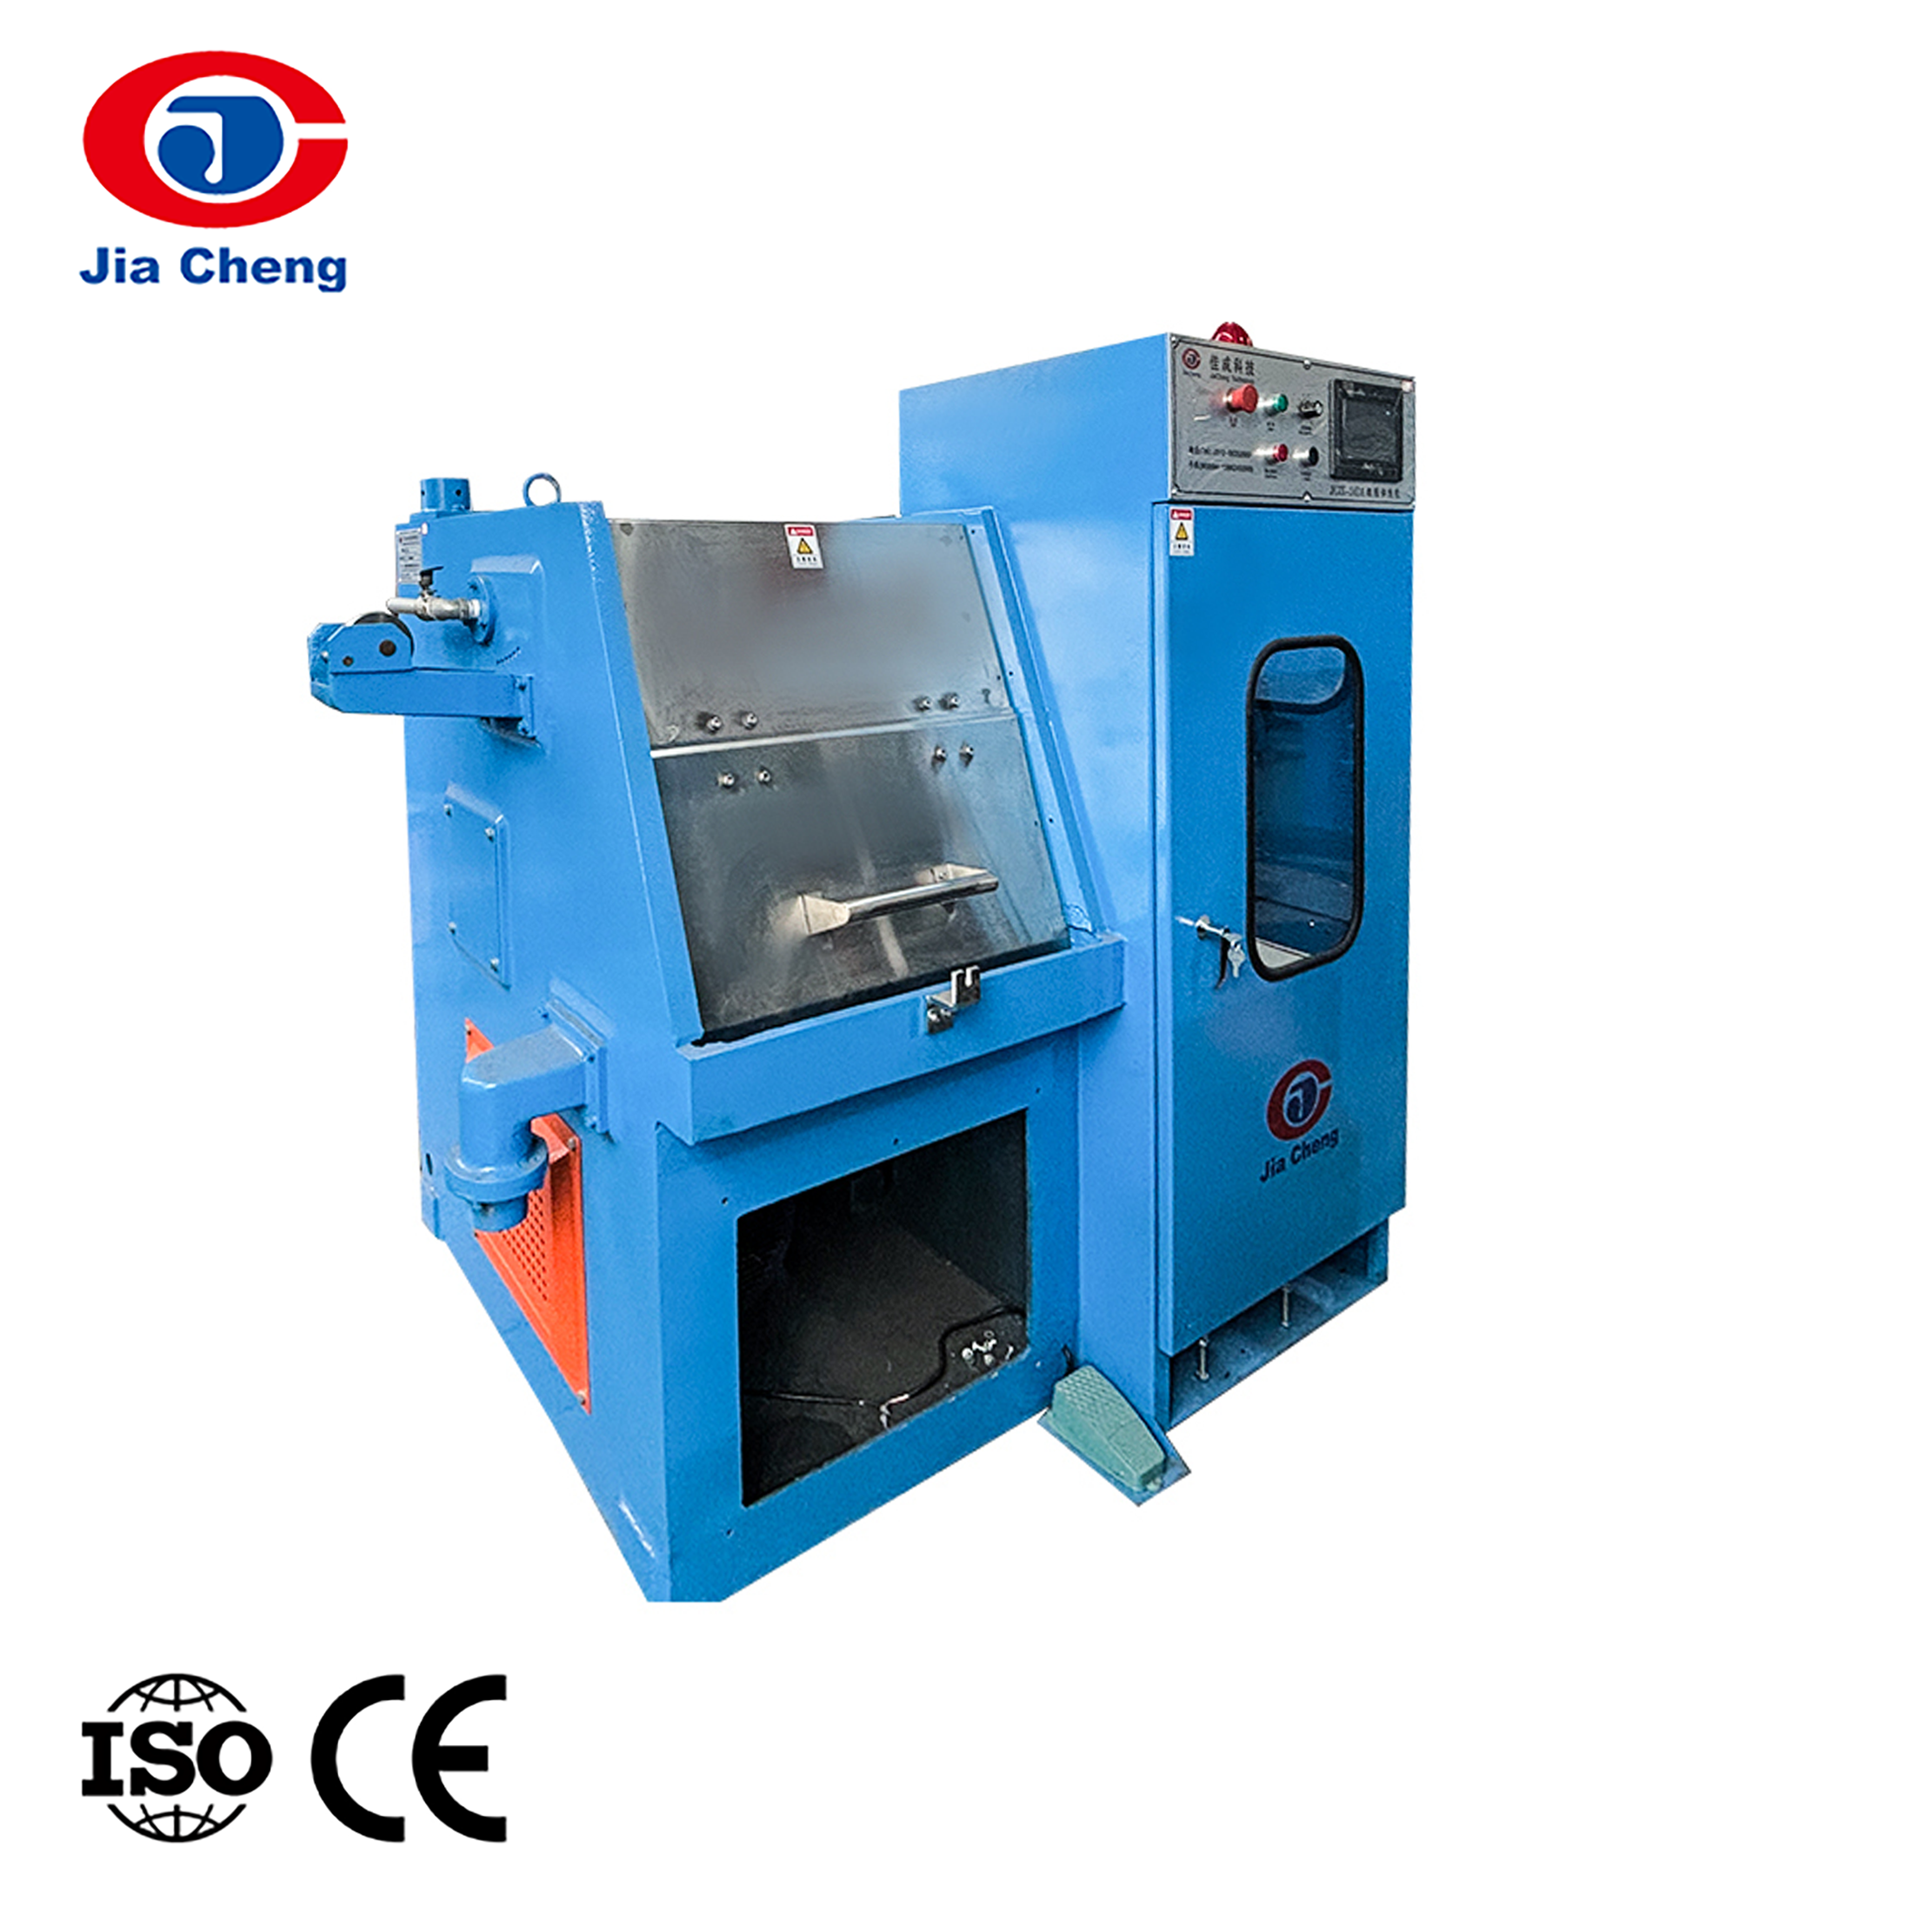
| Fine Wire Drawing Machine (pre-coating) | 2.6mm down to 0.05mm copper/aluminum | up to 15-20 m/s | AC motor, precision tension control | 7.5-30 kW |
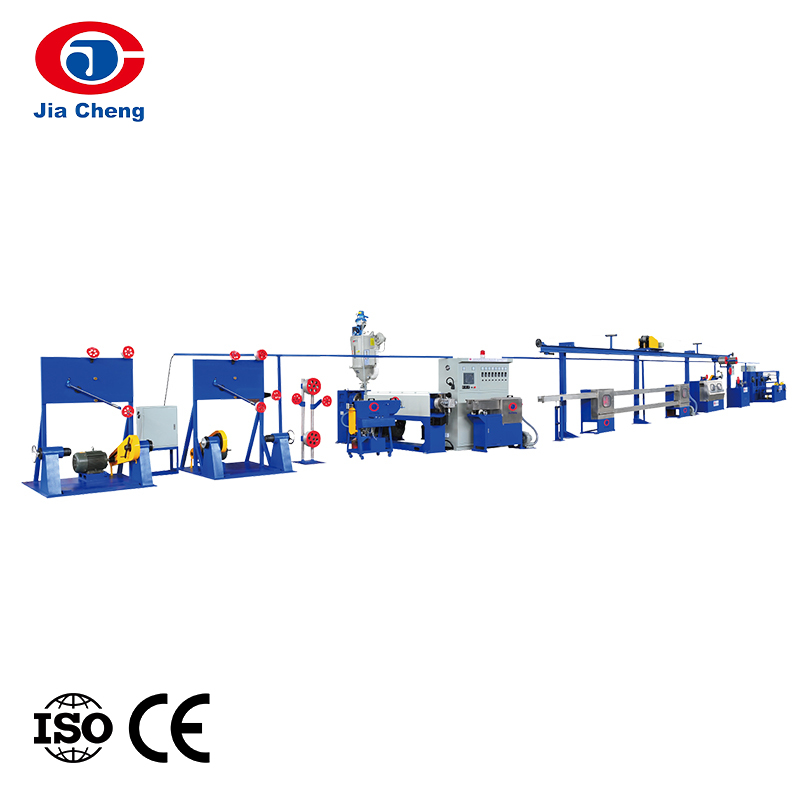
| Vertical Enameling (Coating) Machine | 0.05mm - 2.5mm finished enameled wire | up to 200-600 m/min depending on gauge and coat count | PLC-controlled oven temperature and speed profile | 30-90 kW (oven + drive combined) |
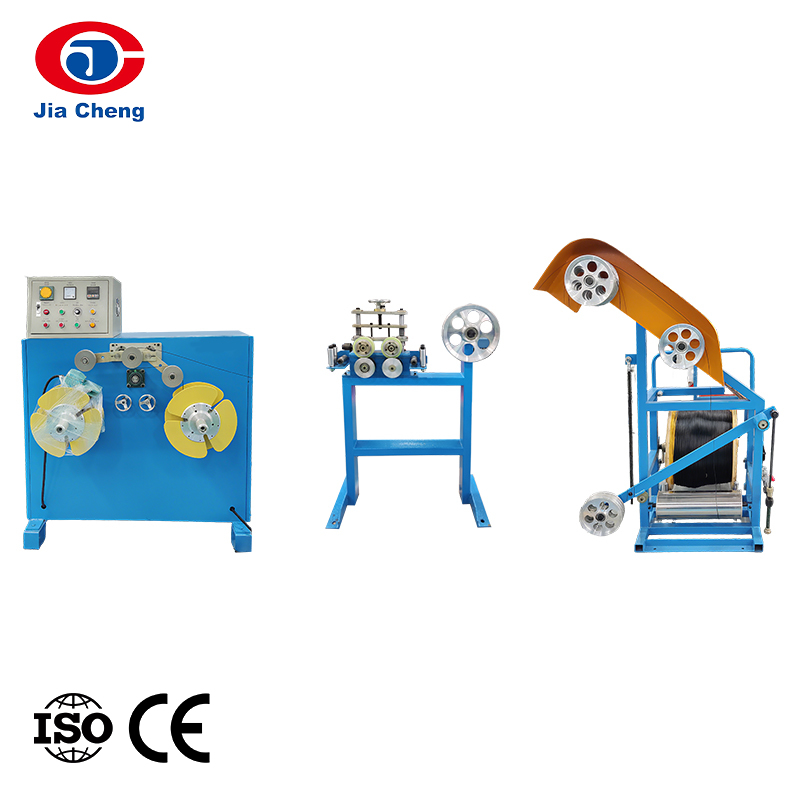
| Automatic Coil Winding/Spooling Machine | coil weight and spool size per local standard | cycle-time dependent | PLC automatic cycle | 3-11 kW |
Finer gauges generally require lower line speeds to allow adequate curing time relative to the thinner, faster-drying coat, while heavier gauges can often run faster with adjusted oven zone temperatures. Share your target wire gauge, enamel type (such as polyurethane, polyester, or polyesterimide), and required insulation class, and we will confirm the appropriate oven length, temperature profile, and line speed for your specification.
We are glad to walk through how these parameter ranges compare to a related material, gauge range, or performance tier you may already be evaluating elsewhere on our site, since many buyers end up comparing more than one processing category before finalizing a production plan. If your target specification falls between two of the ranges shown here, or requires a combination not directly reflected in the table above, share the details and we will confirm a configuration matched specifically to your case rather than asking you to round up to the nearest standard option. We would also rather flag a genuine limitation in what Enameled Wire Production Equipment equipment can reliably achieve early in the conversation than let a mismatched expectation carry through to a formal quotation and cause disappointment later.
Matching Equipment to Your Product Line
Enameled wire buyers typically already know their target wire gauge range and the insulation class or temperature rating their end application requires, since this is usually dictated by the motor or transformer design the wire will go into. Our approach starts from that target specification and works backward to the drawing and coating equipment configuration needed to hit it consistently, since oven length, number of coating passes, and curing temperature all depend directly on your target enamel type and insulation thickness.
For finer magnet wire gauges common in small motor windings, we typically emphasize oven zone precision and lower-speed, higher-quality curing, while for heavier gauges used in larger transformers or motors, output speed becomes a bigger factor alongside insulation consistency. We also discuss whether you need single or dual coating (for example a base enamel layer plus a topcoat for improved lubricity or bonding), since this affects the number of coating passes and oven configuration required.
If you can share your target wire gauge, insulation class or temperature rating, and enamel type, we will propose a drawing and coating line configuration matched to that specification, and flag any aspects of your target output volume that might call for a longer oven or additional coating heads rather than a single standard configuration.
This matching process usually takes a short back-and-forth rather than a single exchange, since buyers often refine their target specification once they see the trade-offs involved in different Enameled Wire Production Equipment configurations. We treat this as a normal, expected part of specifying equipment correctly, and would rather spend extra time confirming the right match up front than have a buyer discover a mismatch only after equipment has already been ordered and shipped. If you already have a detailed specification document from your own customer, an internal engineering team, or an industry standard you need to meet, sending it to us directly is often the fastest way to get an accurate, well-matched proposal, since it removes ambiguity from the technical discussion and lets our engineers respond with specifics rather than general ranges.
Quality Control and Certification
Enameled wire quality is judged on a combination of dielectric strength, coating thickness uniformity, and adhesion/flexibility of the cured enamel layer, all of which are directly affected by oven temperature control and line speed consistency. Our quality process for this equipment category is built around verifying these factors specifically.
Enameling machines are tested with sample wire run through the full coating and curing cycle, and we check coating thickness consistency and surface appearance (freedom from bubbles, pinholes, or uneven buildup) as part of the pre-shipment evaluation. Oven temperature zones are individually calibrated and tested for uniformity, since an uneven temperature profile is one of the most common causes of inconsistent enamel curing and finished wire quality.
We use PLC and drive components from recognized international brands for oven temperature and line speed control, given how directly these affect finished wire quality. If your target application requires enameled wire meeting a specific insulation class or industry standard (referencing IEC or NEMA-type magnet wire specifications, for example), share that with us during quotation so we can confirm our equipment's oven configuration and process control are suited to consistently achieving it.
We document every quality check performed during manufacturing and testing so the records travel with the Enameled Wire Production Equipment you purchase, giving your own quality team a documented baseline to reference once the equipment is running in your facility. If your organization has an internal supplier qualification or quality audit process, we are glad to provide additional documentation or answer specific questions as part of that process, rather than only offering our standard test report. We would rather be transparent about exactly what has and has not been verified before shipment than leave you to assume a broader scope of testing than was actually performed, since that kind of misunderstanding tends to surface at the worst possible time, once the equipment is already installed and running.
Frequently Asked Questions
Q: What enamel types can this equipment apply?
A: Common magnet wire enamels including polyurethane, polyester, and polyesterimide can be applied with appropriate oven temperature and speed settings; share your target enamel type and we will confirm suitability and configuration.
Q: How many coating passes does the wire need?
A: This depends on your target insulation thickness and coating grade requirements, typically ranging from several to over a dozen passes through the enamel bath and oven; we will confirm the appropriate number for your specification.
Q: Can the same line process both copper and aluminum magnet wire?
A: In many cases yes, with appropriate drawing tooling changes upstream of the coating machine; the enameling process itself is similar for both base metals with the same enamel type.
Q: What insulation class can this equipment achieve?
A: This depends on the enamel type and curing process rather than the equipment alone; we can advise on which enamel and oven configuration combinations are needed to reach specific temperature class ratings.
Q: How is coating thickness measured during production?
A: Through periodic sample measurement using standard wire gauge and thickness testing methods; we can advise on recommended in-process testing frequency for your target production volume.
If your question about Enameled Wire Production Equipment is not answered here, reach out directly with your specific situation rather than assuming a general answer applies to your case; because equipment specification depends so heavily on your exact target product, gauge range, and application, many of the most useful answers are specific to your project rather than universal. We would rather take the time to answer a specific question accurately, even if that means asking you a few clarifying questions first, than give a generic response that sounds complete but does not actually apply to what you are trying to build or the standard you need to meet.
Price Range and Quotation Process
Enameled wire equipment typically involves a higher investment than standard wire drawing equipment of comparable gauge range, reflecting the precision oven system, multi-zone temperature control, and enamel application system this equipment requires. Exact pricing depends on your target gauge range, enamel type, number of coating passes, and target output speed.
To prepare a quotation, we typically need your target wire gauge range, enamel type and insulation class, target output, and whether you need integrated fine wire drawing or are feeding the coating machine with pre-drawn wire. With this information we can usually return a formal quotation, including proposed oven configuration and lead time, within a few business days.
If you are a motor or transformer manufacturer considering bringing magnet wire production in-house rather than purchasing finished enameled wire, we are happy to help you think through that comparison — landed wire cost and lead time versus equipment investment and in-house production cost — so you can make an informed decision before committing to equipment.
We recognize that different buyers are at different stages of planning, from early budget research to a final purchasing decision, and we are happy to provide a general pricing indication for Enameled Wire Production Equipment even before you have finalized every technical detail, so you can gauge whether this category of equipment fits your overall project budget before investing more time in a detailed specification. If your budget research is still at an early stage, say so directly and we will tailor the level of detail in our response accordingly, rather than pushing for a full technical exchange before you are ready to have that conversation.